What Is a Magnetic Assembly?
A magnetic assembly combines one or more permanent magnets with supporting parts, such as a steel housing, mounting plate, shaft, or plastic carrier. These parts help position the magnets, protect them from damage, and connect them to the equipment.
For example, a
pot magnet contains a magnet inside a steel cup. The cup protects the magnet and helps concentrate magnetic flux at the working face. A threaded hole or stud provides a practical way to mount the assembly.
Other examples include:
·
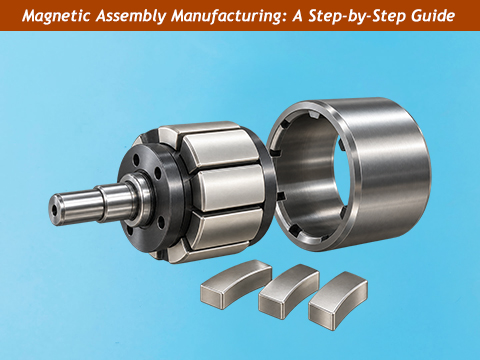
Rotor assemblies that position magnets around a rotating shaft.
·
Magnetic couplings that transfer torque without direct contact between the driving and driven parts.
·
Halbach arrays that arrange magnets to strengthen the field on one side while reducing it on the other.
The performance of a magnetic assembly depends on the complete design. Magnet grade matters, but so do magnet orientation, supporting materials, component alignment, and the gap between the assembly and its working surface. Manufacturing must control these details to deliver consistent results.
Step 1 — Define the Application Requirements
Before choosing a magnet, define what the finished assembly needs to do and where it will operate. Clear requirements help avoid a design that performs well in a sample test but fails in actual use.
Start with these five points:
·
Required magnetic performance: Specify the holding force, transmitted torque, or magnetic field needed for the application. Include the conditions under which it must be measured.
·
Available space and mounting: Provide the maximum dimensions, mounting locations, and mating parts. Identify any limits on weight or access during installation.
·
Working air gap: State the distance between the magnet assembly and the part it acts on. Include paint, protective covers, or other layers that create separation.
·
Operating conditions: Confirm the normal and maximum temperatures, exposure to moisture or chemicals, and expected vibration or impact.
·
Quantity and target cost: Share prototype quantities and expected production volumes. These help determine suitable materials, tooling, and assembly methods.
For example, a holding-force requirement should identify the target steel's material and thickness, the contact gap, and the direction of loading. A force measured under direct contact may not represent performance through a painted surface.
Agreeing on these details early gives the manufacturer a clear basis for design, prototyping, and final testing.
Step 2 — Choose the Right Magnet Material and Grade
The right magnet must deliver the required performance within the assembly's space, temperature, and cost limits. Material, grade, dimensions, and coating should be considered together.
Comparing Magnet Materials
|
Material |
Main advantages |
Key considerations |
|
Neodymium (NdFeB) |
High magnetic strength in a compact size |
Requires suitable corrosion protection and careful grade selection for elevated temperatures |
|
Samarium cobalt (SmCo) |
Good temperature stability and corrosion resistance |
Brittle and generally more expensive |
|
Ferrite |
Economical with good corrosion resistance |
Usually needs more space to achieve comparable magnetic output |
|
Alnico |
Excellent temperature stability and high-temperature capability |
More easily demagnetized; magnetic circuit design needs particular care |
The application determines which balance of properties is most useful. For example, limited space may favor neodymium, while demanding temperature conditions may favor samarium cobalt.
Selecting Grade, Size, and Magnetization Direction
For neodymium magnets, a higher grade number generally indicates greater magnetic energy. Temperature capability also depends on the grade designation, including suffixes such as H or SH. Make sure the
neodymium magnet grade is suitable for the assembly’s operating conditions.
The drawing should also specify:
·
Dimensions and tolerances: Include the space needed for coatings and bonding.
·
Magnetization direction: Identify the required direction through the magnet.
·
Pole arrangement: Show where north and south poles must sit within the assembly.
Two magnets with identical dimensions can produce different field patterns if their magnetization directions differ. Clear pole markings on the drawing help prevent assembly errors.
Choosing a Protective Coating
Sintered neodymium magnets normally need protection against corrosion. Common options include nickel-copper-nickel plating and epoxy coatings. The choice should reflect moisture exposure, chemicals, handling, and the intended bonding process.
Coating thickness must also be included in the finished dimensions. For close-fitting components, specify whether drawing tolerances apply before or after coating.
Step 3 — Design the Housing and Supporting Components
The housing and supporting parts protect the magnets, maintain their position, and connect the assembly to the equipment. In some designs, they also help direct the magnetic field toward the working area.
Choose Materials for Each Component’s Role
Steel components can provide a path for magnetic flux. Their shape and thickness affect how the magnetic circuit performs. Aluminum, brass, or plastic may be suitable for parts that provide support without creating a steel path for the field.
Material selection should also consider mechanical loads, corrosion exposure, weight, and compatibility with neighboring components.
Plan the Fit and Assembly Details
A production drawing should clearly define:
·
Positioning features: Pockets, shoulders, or locating surfaces that keep magnets aligned.
·
Critical tolerances: Dimensions that control magnet spacing, concentricity, or the working air gap.
·
Bonding clearance: Enough space for the specified adhesive layer.
·
Retention and mounting: Features that secure the magnets and attach the assembly to the equipment.
Magnets are brittle, so the design should avoid concentrated loads or excessive fitting pressure. Mounting forces should be carried by suitable supporting components wherever practical.
Check the Design Before Volume Production
Review whether the parts can be machined, coated, assembled, and inspected consistently. Tight tolerances should be reserved for dimensions that affect fit or function.
A prototype then allows the team to verify component fit, assembly access, and magnetic performance before committing to production tooling.
Step 4 — Prepare and Inspect the Components
Before assembly begins, check that the magnets and supporting parts match the approved drawings. Finding defects at this stage helps prevent rework after magnets have been bonded or enclosed.
Preparation should cover four areas:
·
Inspect the magnets: Check dimensions, coating condition, cracks, and chipped edges against the acceptance criteria. For pre-magnetized parts, verify polarity and magnetization direction.
·
Check the supporting parts: Inspect housing dimensions, locating features, and mounting holes. Remove burrs or debris that could prevent correct seating or damage the magnet coating.
·
Clean the bonding surfaces: Remove oil, dust, and other contamination using a cleaning method compatible with the coating and adhesive. Allow surfaces to dry before bonding, and avoid touching prepared areas.
·
Prepare the assembly fixtures: Confirm that fixtures locate the parts correctly and maintain the required spacing. They should allow controlled placement without forcing brittle magnets into position.
Keep inspected components identified by part number and batch, particularly when similar-looking magnets have different grades or pole arrangements.
The aim is to give the assembly team clean, verified parts that fit correctly and can be positioned consistently.
Step 5 — Assemble and Magnetize the Magnetic Assembly
During assembly, magnets are placed in position, secured, and magnetized according to the approved design.
Secure the Magnets
Three common methods are used:
·
Adhesive bonding: Glues magnets to the housing or other components.
·
Mechanical retention: Uses sleeves, retaining plates, or other features to hold magnets in place.
·
Potting: Surrounds magnets with a protective compound for added support and protection.
Some assemblies combine methods. For example, a rotor may use both adhesive and a retaining sleeve.
Control Position and Polarity
Fixtures hold magnets at the correct angle and spacing. For pre-magnetized parts, they also help control attraction and repulsion during placement.
Check each magnet’s pole orientation before fixing it permanently. For bonded parts, control the adhesive amount and layer thickness to maintain the correct fit.
Plan Curing and Magnetization
Keep bonded components in position for the required curing time. If heat is used, confirm that the curing temperature is suitable for the magnets, coatings, and other parts.
Magnets can be magnetized
before or after assembly. Using unmagnetized parts can make assembly easier, but magnetizing the finished unit requires suitable equipment and a compatible design. Confirm the method before production begins.
Step 6 — Test the Finished Magnetic Assembly
Final inspection confirms that the assembly meets the approved drawing and performance requirements. Testing should reflect how the product will be used.
Key checks include:
·
Dimensions and fit: Check overall size, mounting features, and critical component positions.
·
Polarity: Confirm that north and south poles match the specified arrangement.
·
Magnetic performance: Measure pull force for holding assemblies, transmitted torque for couplings, or magnetic field strength at specified locations.
·
Magnet retention: Verify that magnets remain secure under the agreed mechanical loads.
·
Environmental durability: Where required, test resistance to temperature changes, moisture, chemicals, or vibration.
Test conditions must be clearly defined. For example, a pull-force result depends on the target steel, surface condition, air gap, and pulling direction. Measurements should use the same agreed setup so results can be compared consistently.
Separate routine production checks from qualification tests. Dimensions, polarity, and selected performance checks may be inspected during production, while longer environmental or destructive tests are typically performed on agreed samples.
Record the results against clear acceptance limits and retain batch identification so any quality issue can be traced.
What Should Buyers Provide for a Custom Magnetic Assembly?
A clear inquiry helps us review feasibility and prepare an accurate quotation. Include the following information where available:
·
Application: Explain what the assembly does and where it will operate.
·
Drawings or CAD files: Show overall dimensions, mounting features, mating parts, and critical tolerances.
·
Performance requirements: Specify the required holding force, torque, or magnetic field, including the working gap.
·
Operating conditions: Provide temperature limits and details of moisture, chemicals, vibration, or impact.
·
Quantity and schedule: State the prototype quantity, expected annual demand, and required delivery date.
·
Testing requirements: Identify acceptance limits, test methods, and any inspection reports needed.
If the design already specifies the magnet material, grade, coating, or pole arrangement, include those details too.
You do not need a finished design to start a discussion. At AEMagnets, we can review your application and available drawings, then help clarify the specifications needed to move toward a prototype.
Conclusion
A well-made magnetic assembly delivers the required performance at a practical production cost. Reaching that balance means choosing materials, tolerances, and assembly methods around the product’s actual function.
Early collaboration between the buyer and manufacturer helps resolve trade-offs while the design is still easy to adjust. This creates a smoother path from the first prototype to repeat orders.
At AEMagnets, we can review your drawings and application requirements to help develop a magnetic assembly suited to your production needs.